NEWS

LATEST How to Reduce Crusher Wear Part Costs

Crusher wear parts are one of the most important operating costs in mining, quarrying, and aggregate production.

Jaw plates, cone crusher liners, mantles, concaves, blow bars, and other wear components are continuously exposed to high impact, compression, and abrasion. In hard-rock applications, poor operating conditions can shorten wear-part life significantly and lead to frequent replacements, production interruptions, and higher maintenance costs.

However, high wear costs are not always unavoidable.

By improving crusher selection, feed conditions, operating parameters, maintenance practices, and wear-part management, operators can often extend wear life and reduce the cost per ton of finished material.

This guide explains practical ways to reduce crusher wear part costs without sacrificing production or product quality.

1. Understand What Is Causing Wear

Before trying to reduce wear-part costs, determine why the parts are wearing.

Different materials create different wear patterns.

Common factors include:

  • Material hardness

  • Abrasiveness

  • Feed size

  • Material shape

  • Moisture and clay content

  • Crushing ratio

  • Crusher operating speed

  • Closed-side setting (CSS)

  • Feed distribution

  • Chamber selection

  • Operating hours

For example, granite and basalt can cause significantly more abrasive wear than many softer limestone applications.

Iron ore and other metallic ores can also create demanding operating conditions.

The first step should therefore be to identify the actual wear mechanism rather than simply replacing parts with a different material.

2. Choose the Right Wear Part for the Application

There is no single wear-part material that is ideal for every crushing application.

The correct choice depends on the material and crushing stage.

For example, jaw crusher wear parts may include different grades and profiles of manganese steel, while cone crusher liners are available in different designs for different feed and product conditions.

When selecting wear parts, consider:

  • Material hardness

  • Abrasiveness

  • Feed size

  • Crusher type

  • Crushing stage

  • Expected production

  • Required product size

  • Operating conditions

A wear part with a higher purchase price may provide a lower total cost if it lasts significantly longer.

The correct comparison is therefore not:

Price per wear part

but:

Wear-part cost per ton

3. Calculate Wear Cost per Ton

One of the simplest ways to evaluate wear-part performance is to calculate the cost per ton.

A basic formula is:

Wear Part Cost per Ton = Total Wear Part Cost ÷ Tons Produced

For example, suppose a cone crusher uses a liner set costing $10,000 and produces 50,000 tons before replacement.

The wear cost is:

$10,000 ÷ 50,000 tons = $0.20/ton

If a different liner costs $12,000 but lasts for 75,000 tons:

$12,000 ÷ 75,000 tons = $0.16/ton

Although the second liner costs more to purchase, its cost per ton is lower.

This is why purchasing decisions should be based on total operating economics rather than the lowest initial price.

4. Keep the Crusher Properly Fed

Uneven feeding is one of the most common causes of inefficient crushing and irregular wear.

A crusher should ideally receive a consistent feed across the crushing chamber.

Poor feeding can result in:

  • Localized liner wear

  • Reduced crushing efficiency

  • Increased vibration

  • Lower throughput

  • Unstable product size

  • Higher energy consumption

For cone crushers, maintaining a proper choke-fed condition can help distribute crushing forces more evenly and improve liner utilization.

For jaw crushers, a stable feed rate and suitable feed distribution can help prevent excessive wear on specific sections of the jaw plates.

5. Avoid Oversized Feed

Sending material larger than the crusher's recommended feed size can dramatically increase mechanical stress.

Oversized rocks can cause:

  • Higher impact loads

  • Uneven wear

  • Crusher blockages

  • Reduced capacity

  • Increased power consumption

  • Damage to components

The blasting, loading, and primary crushing processes should therefore be coordinated.

If the feed contains too much oversized material, improving upstream rock fragmentation may sometimes reduce downstream wear costs.

In other words, wear management does not start at the crusher. It starts at the mine face or quarry face.

6. Control the Closed-Side Setting

The closed-side setting (CSS) has a direct influence on crusher performance and wear.

If the setting is too small, the crusher may experience:

  • Higher crushing forces

  • Increased power consumption

  • Higher wear rates

  • Greater risk of operating outside the recommended conditions

If the setting is too large, the crusher may produce insufficient reduction and increase the load on downstream equipment.

The correct CSS should balance:

Capacity + Product Size + Energy Consumption + Wear Life

Operators should avoid changing the setting simply to increase production without considering the effect on wear.

7. Use the Correct Crushing Chamber

Cone crusher chamber selection has a major impact on wear-part performance.

The chamber should match:

  • Feed size

  • Feed gradation

  • Required product size

  • Material characteristics

  • Crusher operating conditions

A chamber that is poorly matched to the application may produce an unfavorable crushing profile and accelerate liner wear.

For example, a chamber designed for finer crushing may not be the best choice for a large feed application.

Proper chamber selection can improve both product quality and wear-part utilization.

8. Maintain Proper Feed Gradation

Feed gradation is another important factor.

A crusher does not process only one particle size in real-world operation. The feed normally contains a range of particle sizes.

If the feed contains too much fine material, the crushing chamber may behave differently from the intended design.

If the feed contains too much coarse material, crushing forces can increase.

A properly designed screening and scalping system can help control the feed entering the crusher.

This may reduce unnecessary crushing and improve wear distribution.

9. Remove Sticky Fines and Clay When Necessary

Moisture and clay can create problems in crushing and screening circuits.

Sticky material may:

  • Block the feed opening

  • Reduce effective chamber volume

  • Increase circulating load

  • Reduce screening efficiency

  • Cause uneven crushing

  • Increase maintenance requirements

If the raw material contains a significant amount of clay or sticky fines, a suitable scalping or washing process may be required.

Removing unwanted fines before crushing can prevent the crusher from spending energy crushing material that does not need further size reduction.

10. Do Not Operate the Crusher Empty or Underloaded

Crusher operating conditions affect wear distribution.

Running a crusher continuously below its appropriate operating range may result in poor crushing conditions and uneven wear.

For cone crushers in particular, maintaining a suitable feed level and consistent material flow helps the crushing chamber work as intended.

The goal is not simply to keep the crusher running.

The goal is to keep it running under stable and appropriate operating conditions.

11. Inspect Wear Parts Regularly

Regular inspection can prevent small wear problems from becoming expensive failures.

Operators should monitor:

  • Liner thickness

  • Jaw plate profile

  • Mantle and concave wear

  • Blow bar condition

  • Wear distribution

  • Cracks

  • Loose components

  • Unusual vibration

  • Changes in product size

Replacing a wear part at the appropriate point is generally better than waiting until it fails completely.

However, replacing it too early also wastes useful material.

A practical maintenance strategy should therefore establish a replacement threshold based on actual operating experience and manufacturer recommendations.

12. Rotate or Reposition Wear Parts When Appropriate

Some wear components can be rotated, reversed, or repositioned depending on the crusher design.

For example, certain jaw plates can be turned around to make better use of the remaining wear material.

This can help achieve more uniform wear and extend the useful life of the component.

However, not every wear part can be rotated or reused.

Operators should follow the crusher manufacturer's maintenance instructions and inspect the part before deciding whether repositioning is appropriate.

13. Keep the Crushing Chamber Properly Lined

Incorrectly installed or poorly fitted wear parts can create uneven loading.

Before operation, check:

  • Correct liner type

  • Correct installation

  • Proper fastening

  • Contact surfaces

  • Bolts and locking systems

  • Clearance

  • Crusher alignment

A small installation problem can become a major maintenance issue after thousands of tons of material have passed through the crusher.

Proper installation is therefore part of wear-cost management.

14. Maintain the Crusher Properly

Wear parts do not operate independently of the crusher.

Poor maintenance of bearings, lubrication systems, hydraulic systems, or other components can indirectly increase wear.

Regular maintenance should include:

  • Lubrication checks

  • Hydraulic system inspection

  • Bearing inspection

  • Drive system inspection

  • Fastener checks

  • Temperature monitoring

  • Vibration monitoring

  • Crusher chamber inspection

A crusher operating outside normal mechanical conditions may consume wear parts faster than expected.

15. Monitor Power and Production Data

Modern crushing plants can use operating data to identify abnormal conditions.

Useful data may include:

  • Tons per hour

  • Motor power

  • Crusher pressure

  • CSS

  • Feed rate

  • Product size

  • Operating hours

  • Wear-part life

For example, if power consumption suddenly increases while production remains unchanged, this may indicate a feed or crushing-condition problem.

Tracking these parameters over time can help operators identify trends before they become major failures.

16. Reduce Unnecessary Recirculating Load

Closed-circuit crushing is common in aggregate and mining plants.

A typical process is:

Crusher → Vibrating Screen → Oversize Return → Crusher

Some circulating load is normal.

However, poor screening efficiency, incorrect crusher settings, or excessive oversize can increase the amount of material returning to the crusher.

Higher circulating load means more material passes through the crusher multiple times.

This can increase:

  • Wear

  • Energy consumption

  • Crusher loading

  • Conveyor loading

Improving screen efficiency and crusher settings can therefore reduce unnecessary wear.

17. Match the Crusher to the Required Production

A crusher that is too small for the required production may operate continuously under excessive load.

This can increase wear and maintenance costs.

On the other hand, installing a crusher that is much larger than necessary can increase capital and operating costs without providing meaningful benefits.

The correct selection should consider:

  • Required TPH

  • Feed size

  • Material characteristics

  • Reduction ratio

  • Final product size

  • Operating hours

  • Expected future production

A properly sized crushing plant generally provides more stable operating conditions.

18. Consider the Whole Crushing Circuit

Wear costs should not be evaluated only at the crusher.

For example:

Feeding → Primary Crushing → Secondary Crushing → Screening → Tertiary Crushing → Final Products

A problem in one stage can increase the workload of another.

If the primary crusher produces excessive oversize, the secondary crusher may experience increased loading.

If the screen performs poorly, the crusher may process more material than necessary.

If the final product requirements are too strict, the circulating load may increase.

Whole-plant optimization is therefore often more effective than optimizing one crusher in isolation.

19. Keep Critical Wear Parts in Stock

Unexpected wear-part failures can result in expensive downtime.

For critical crushing equipment, it is useful to maintain an appropriate inventory of:

  • Jaw plates

  • Mantles

  • Concaves

  • Blow bars

  • Screen media

  • Bolts and fastening components

  • Other critical replacement parts

The correct inventory level depends on lead time, production schedule, wear rate, and supplier availability.

The objective is not to hold excessive inventory, but to avoid a situation where a relatively inexpensive wear part stops a high-value production line for several days.

20. Compare Suppliers Based on Total Cost

When purchasing wear parts, price should not be the only selection criterion.

Compare suppliers based on:

  • Wear life

  • Material quality

  • Manufacturing consistency

  • Fit and installation

  • Delivery time

  • Technical support

  • Warranty

  • Cost per ton

A lower-cost liner that lasts 30% less time may be more expensive in the long run.

The best supplier evaluation should therefore use actual production data whenever possible.

A Practical Wear-Cost Optimization Strategy

A simple improvement process can be organized into five steps:

Step 1: Record Current Wear Performance

Record the purchase price, service life, tons produced, and replacement frequency of each major wear component.

Step 2: Calculate Cost per Ton

Compare different wear-part types using actual production data.

Step 3: Identify the Main Cause of Wear

Check feed size, abrasiveness, CSS, chamber selection, feed distribution, and operating conditions.

Step 4: Improve Operating Conditions

Optimize feeding, screening, crusher settings, and maintenance.

Step 5: Compare Results

After changing the operating conditions or wear parts, measure the actual service life and cost per ton.

This creates a continuous improvement cycle rather than relying on assumptions.

Example: Reducing Cone Crusher Liner Costs

Suppose a cone crusher produces 400 TPH and operates for 10 hours per day.

Daily production is:

400 × 10 = 4,000 tons/day

If one liner set lasts 30 days:

4,000 × 30 = 120,000 tons

If the liner set costs $18,000:

$18,000 ÷ 120,000 = $0.15/ton

Now suppose better feed distribution and optimized operating parameters increase liner life to 36 days.

Production becomes:

4,000 × 36 = 144,000 tons

The new wear cost is:

$18,000 ÷ 144,000 = $0.125/ton

The difference is:

$0.15 − $0.125 = $0.025/ton

At 120,000 tons, this represents approximately:

$3,000 of wear-part cost reduction

This example shows why relatively small improvements in liner life can have a meaningful effect on large-volume crushing operations.

The Most Important Factors Affecting Wear-Part Costs

In practice, the major factors can be summarized as follows:

FactorPotential Impact on Wear
Material abrasivenessHigh
Incorrect feed sizeHigh
Uneven feedingHigh
Incorrect CSSHigh
Poor chamber selectionHigh
Excessive circulating loadHigh
Poor maintenanceMedium to High
Incorrect wear materialHigh
Poor installationMedium to High
Inefficient screeningMedium
Unstable operating conditionsHigh

The actual impact varies from one application to another.

Final Thoughts

Reducing crusher wear-part costs is not simply about buying cheaper liners or jaw plates.

The biggest savings often come from improving the way the entire crushing system operates.

A practical strategy is to:

Select the right wear parts → Control feed conditions → Optimize crusher settings → Maintain stable feeding → Improve screening → Inspect regularly → Track cost per ton

For hard and abrasive materials, even a small improvement in wear life can generate significant savings when the plant produces hundreds of thousands or millions of tons per year.

The key metric should always be total wear cost per ton, supported by real production and maintenance data.

Frequently Asked Questions

How can I make crusher liners last longer?

Maintain stable feeding, avoid oversized material, use the correct chamber and liner profile, optimize the crusher setting, monitor wear regularly, and keep the crusher properly maintained.

What causes excessive jaw plate wear?

Common causes include abrasive material, uneven feeding, oversized feed, unsuitable jaw plate profiles, incorrect operating conditions, and poor feed distribution.

How often should crusher wear parts be replaced?

There is no universal replacement interval. Replacement should be based on actual wear measurements, production volume, crusher performance, and the manufacturer's recommended limits.

Is a more expensive wear part always better?

No. The most important factor is the total cost per ton. A more expensive wear part may be more economical if it provides significantly longer service life.

How do I calculate crusher wear cost per ton?

Divide the total cost of the wear part by the tons produced during its service life:

Wear Cost per Ton = Wear Part Cost ÷ Production During Service Life

Can crusher settings affect wear life?

Yes. Incorrect settings can increase crushing forces, reduce efficiency, increase circulating load, or create unfavorable wear patterns. Settings should be optimized for the material and required product size.
Previous News

21/5/2026

21/5/2026

Beyond Crushing: How to Optimize Your Mineral Processing Circuit for Maximum Recovery

Achieving maximum mineral recovery requires a holistic approach that optimizes the entire processing circuit, not just crushing. Here’s a practical guide to systematically enhance recovery across all stages.

1. Optimize Comminution: The Foundation of Liberation

The goal is to achieve optimal mineral liberation with minimal energy. The principle of "more crushing, less grinding" is key.

  • Feed Size Management: Install a scalping screen before the primary crusher to remove fines. This prevents "packing" in the crusher chamber and can increase primary crushing capacity by 20-30%.

  • Balanced Crushing Ratios: Distribute size reduction across multiple stages (primary, secondary, tertiary) to keep each machine in its efficiency "sweet spot".

  • Grinding Stability: Maintain stable feed rate, pulp density, and circulating load. Use online power draw and pressure data for control instead of rule-of-thumb adjustments to prevent under- or over-grinding.

  • Advanced Equipment: Consider High-Pressure Grinding Rolls (HPGR) for energy savings (20-40% less grinding power) and to generate micro-cracks that can improve downstream leaching recovery by 3-8%.

2. Enhance Separation: Target the Valuable Minerals

Separation efficiency directly dictates final recovery.

  • Flotation Circuit Design: Implement well-configured rougher, cleaner, and scavenger stages. Circuits with recycle streams often yield better rougher stage recovery. Modern flotation cells with advanced mechanisms (like deep vane designs) and smart control systems can significantly cut costs and boost efficiency.

  • Reagent & Chemistry Control: Precisely manage pH, collector, and frother dosage. For example, spodumene flotation is optimal in a pH range of 6.5-7.5. Water chemistry is critical, especially in water-scarce areas.

  • Incorporate Pre-concentration: Use methods like Dense Media Separation (DMS) or sensor-based sorting (e.g., XRT) early in the circuit to reject waste rock (up to 30-50% throw-away rate), reducing energy and load on downstream processes.

  • Apply Gravity for Coarse Gold: Install gravity recovery units like jigs or shaking tables in the grinding circuit to capture fast-settling, coarse gold particles before they are over-ground or lost.

3. Improve Solid-Liquid Separation: Minimize Losses in Tailings

Efficient washing and thickening are crucial for leach circuits.

  • Counter Current Decantation (CCD) Optimization: Using high-density or paste thickeners instead of conventional high-rate thickeners can be more cost-effective. Recovery in a CCD circuit is controlled by the number of stages, liquid split, and mixing efficiency. Optimizing these can push recovery from 86% to over 95%.

4. Leverage Digitalization & Advanced Control

Data-driven optimization is now a game-changer.

  • Advanced Process Control (APC): Model Predictive Control (MPC) systems provide superior regulation for complex processes like SAG mill loading and flotation levels, maintaining stability and optimal setpoints better than traditional PID loops.

  • AI-Powered Optimization: AI models can learn non-linear relationships between process variables (e.g., reagent dosage, bubble size, mill speed) and tune them in real-time to maximize recovery. This can lead to an average 1-3% increase in metal recovery and 5-10% savings in grinding energy.

  • Real-time Monitoring: Use froth cameras (e.g., VisioFroth™) for online analysis of bubble size, velocity, and stability to optimize reagent addition and flow control.

Key Takeaways for Maximum Recovery

  • System View: Treat the entire circuit as an interconnected system. A bottleneck in crushing limits grinding, which limits separation.

  • Liberation First: Ensure optimal and consistent particle size from comminution. This sets the upper limit for recovery.

  • Stage-appropriate Technology: Choose the right separation method (flotation, gravity, magnetic) based on mineralogy.

  • Embrace Data: Move from experience-based to data-driven control. Implement sensors, APC, and consider AI for closed-loop optimization.

  • Continuous Testing: Conduct regular metallurgical testing and pilot studies to adapt to ore variability and test new strategies.

By focusing on these interconnected areas—efficient size reduction, targeted separation, effective dewatering, and intelligent control—you can systematically push your mineral processing circuit toward its maximum recovery potential.


14/5/2026

14/5/2026

Taming Hard Rock: A Guide to Durable and Efficient Crushing Circuits for Granite and Basalt

Processing granite and basalt—rocks with Mohs hardness of 6-7 and compressive strength often exceeding 150 MPa—demands a crushing circuit built for extreme abrasion and impact. A well-designed system balances throughput, product shape, and long-term operating costs. Here’s a practical guide based on proven industry configurations.

1. Core Challenges & Design Philosophy

  • High Abrasiveness: Rapid wear of liners and components is the primary cost driver. Equipment selection must prioritize wear resistance over initial price.

  • Impact Loads: Primary crushers must withstand repeated shock from large, hard feed.

  • Product Shape: Cubical aggregates are essential for high-value applications like concrete and asphalt; excessive flakiness reduces marketability.

  • System Stability: Consistent feed and closed-side settings (CSS) are critical to maintain throughput and product gradation.

2. Equipment Selection: The Hard-Rock Hierarchy

Stage

Recommended Equipment

Key Considerations for Granite/Basalt

Primary

Heavy-duty jaw crusher (tracked or stationary)

• Wide feed opening (≥700mm) to accept large blasted rock.
• High manganese steel or alloy liners optimized for abrasion.
• Robust frame to handle impact loads; expected liner life: 120,000–180,000 tons .

Secondary

Multi-cylinder hydraulic cone crusher

• Inter-particle compression crushing produces cubical product with low flakiness (<8%).
• Hydraulic adjustment allows real-time CSS tuning for different product specs.
• Far superior wear life vs. impact crushers on abrasive stone .

Tertiary/Shaping

Short-head cone crusher or VSI (selectively)

• Cone crusher for strict gradation control and lower wear cost.
• VSI can enhance cubicity but may incur higher wear on high-silica basalt.

Screening

3- or 4-deck vibrating screen with closed-circuit return

• 3-deck screens produce 3–4 saleable fractions + oversize return.
• 4-deck screens offer greater flexibility for tight spec products (e.g., 0–3, 3–8, 8–16, 16–22 mm) .

Feeding & Conveying

Vibrating grizzly feeder (with pre-screen) + heavy-duty conveyors

• Pre-screening removes fines to reduce wear and improve capacity.
• Steady, non-surge feeding is critical to liner life and throughput.

3. Process Flow: Proven Configurations

A. Classic Hard-Rock Closed Circuit (Most Common)

Vibrating Feeder → Jaw Crusher (Primary) → Cone Crusher (Secondary) → Screen → (Oversize return to cone)
  • Best for: 200–400 TPH plants producing standard concrete/asphalt aggregates (0–5, 5–10, 10–20, 20–31.5 mm) .

  • Why it works: Jaw handles coarse reduction; cone provides stable, shape-controlled secondary crushing; closed circuit maximizes yield and consistency.

B. Mobile “Sweet-Spot” Line (200–300 TPH)

  • Configuration: Tracked jaw + tracked cone + tracked 3‑deck screen .

  • Advantages: High mobility, fast commissioning, ideal for multi‑site contractors or quarries with moving faces.

  • Output recipes: Adjustable for road base, mixed aggregates, or premium asphalt mixes.

C. Large‑Scale Fixed Plant (600–700 TPH)

  • Flow: Jaw (PE‑1200×1500) → 2× cone crushers (HPC400) → VSI shaping → multi‑deck screening .

  • Use case: Major infrastructure projects requiring high‑volume, spec‑grade aggregates.

4. Key Design & Operational Tips

  • Capacity “Sweet Spot”: For mobile setups, 200–300 TPH offers the best balance of throughput, logistics, and flexibility .

  • Wear Management:

    • Monitor liner thickness every 250 operating hours; cone mantles typically last 450–600 hours on granite .

    • Use condition‑monitoring systems to plan replacements during scheduled downtime.

  • Dust Control: Fully enclosed conveying + centralized bag‑filter systems keep emissions below 20 mg/m³ .

  • Automation: PLC control systems monitor current, temperature, and vibration, enabling real‑time CSS adjustment and reducing changeover time by up to 80% .

  • Power Options: Diesel‑electric hybrid drives are ideal for remote hard‑rock sites without stable grid power .

5. Configuration Examples by Output Goal

Target Product

Recommended Flow

Key Equipment

Typical Capacity

Coarse aggregates (0–150 mm)

Primary only

Jaw crusher + feeder

150–250 TPH

Concrete/asphalt mixes

Jaw → Cone → 3‑deck screen

Jaw + multi‑cylinder cone + closed‑circuit screen

200–350 TPH

Premium cubical aggregates

Jaw → Cone → VSI → 4‑deck screen

Jaw + cone + shaping crusher + multi‑deck screen

250–400 TPH

High‑spec railway ballast

Closed‑circuit with precise screening

Jaw + cone + screen with strict return loop

300–500 TPH

6. Bottom Line

A durable, efficient hard‑rock circuit starts with a heavy‑duty jaw crusher for primary reduction, followed by a hydraulic cone crusher for secondary shaping—avoid impact crushers for highly abrasive granite/basalt. Closed‑circuit screening with return conveyors ensures gradation control and maximizes yield. For most quarry operators, a 200–300 TPH mobile jaw‑cone‑screen train provides the optimal blend of performance, mobility, and cost‑effectiveness . Remember: consistent feeding, proper CSS settings, and proactive wear‑part management are just as critical as equipment selection itself.

Need a tailored solution? Share your feed size, target products, and site conditions for a specific circuit recommendation.


8/5/2026

8/5/2026

How to Turn Demolished Concrete into High-Quality Recycled Aggregate

Every year, billions of tons of construction and demolition (C&D) waste are generated globally. Simply landfilling it wastes precious space, resources, and harms the environment. So, how can we transform this discarded concrete and rubble into a valuable resource? The answer lies in an efficient C&D waste crushing and screening plant.

The Core Solution: Mobile Crushing and Screening Stations

For scattered demolition sites, mobile crushing and screening stations are the ideal choice. They can be driven directly to the site, processing waste on the spot and eliminating high transport costs.

  1. Pre-Sorting and Feeding: Wood, plastic, and other impurities are removed via manual or mechanical sorting. The remaining concrete blocks are evenly fed into the crusher by a feeder.

  2. The Core Crushing Stage: A jaw crusher is typically used for primary crushing, breaking down large concrete chunks. Next, an impact crusher or cone crusher handles secondary crushing. Impact crushers produce well-shaped aggregate, ideal for road base materials. For higher demands on particle shape and hardness, a cone crusher is preferred.

  3. De-ironing and Screening: A magnetic separator removes rebar during crushing. Subsequently, a vibrating screen classifies the material into different specifications (e.g., 0-5mm, 5-10mm, 10-31.5mm), producing clean recycled coarse and fine aggregate.

  4. Final Application: This recycled aggregate can be used for road sub-bases, backfill, producing recycled bricks, concrete blocks, and even in some non-structural concrete, closing the resource loop.

The Investment Value: It not only solves waste disposal problems but also creates a new revenue stream, helps companies obtain green building certifications, and enhances their social responsibility profile.


30/4/2026

30/4/2026

Granite Crushing Plant Design for High Output

Granite is one of the hardest and most durable natural stones, widely used in construction, infrastructure, and decorative projects. Achieving high output while maintaining product quality requires a carefully designed crushing plant. This article explores the key considerations in designing a granite crushing plant that maximizes productivity, minimizes operational costs, and ensures consistent product quality.

Understanding Granite Properties

Before designing a crushing plant, it is essential to understand granite’s physical properties:

  • Hardness: Granite is extremely hard (Mohs hardness of 6–7), which affects the choice of crusher types.

  • Abrasion Resistance: High silica content can accelerate wear on crushing equipment.

  • Size and Shape: Granite blocks vary in size, influencing feeder, crusher, and conveyor selection.

Knowing these factors helps in selecting suitable crushers, screens, and conveyors that can handle high-volume operations.

Key Components of a High-Output Granite Crushing Plant

  1. Primary Crusher
    Jaw crushers or gyratory crushers are preferred for coarse crushing of granite. They provide high throughput and can handle large boulders with minimal breakdowns.

  2. Secondary Crusher
    Cone crushers or impact crushers are ideal for medium to fine crushing. They enhance product uniformity and are suitable for shaping aggregates for construction projects.

  3. Screening System
    Multi-deck vibrating screens separate crushed granite into different size fractions. Proper screening ensures consistent particle size and reduces recirculation, improving efficiency.

  4. Conveying Equipment
    Belt conveyors connect each stage of the crushing process. Efficient conveyor design minimizes material spillage and ensures smooth flow, reducing downtime.

  5. Dust and Noise Control
    Enclosures, dust collectors, and water sprays reduce environmental impact and comply with local regulations, which is particularly important in urban or sensitive areas.

Design Strategies for Maximum Output

  • Optimized Layout: Position crushers, screens, and conveyors to minimize material handling and travel distance.

  • Automated Controls: Use PLC and sensor-based systems to monitor feed rate, crusher load, and output quality. Automation reduces human error and increases throughput.

  • High-Capacity Equipment: Select crushers and screens with capacities exceeding the expected production target to accommodate peak demand.

  • Regular Maintenance: Schedule preventive maintenance for wear parts to avoid unexpected downtime and maintain consistent output.

Local Considerations for GEO Optimization

When designing a granite crushing plant, location-specific factors influence performance:

  • Availability of Granite Deposits: Proximity to quarries reduces transportation costs.

  • Local Labor and Utilities: Access to skilled operators, electricity, and water is critical.

  • Environmental Regulations: Compliance with local dust, noise, and wastewater standards ensures uninterrupted operations.

Understanding these factors helps engineers design a plant that not only achieves high output but also operates sustainably in its local environment.

Conclusion

A high-output granite crushing plant requires careful planning, robust equipment, and efficient workflows. By integrating the right crushers, screening systems, conveyors, and automation technologies, operators can maximize productivity while maintaining high-quality granite aggregates. Attention to local conditions ensures compliance and long-term operational efficiency.


24/4/2026

24/4/2026

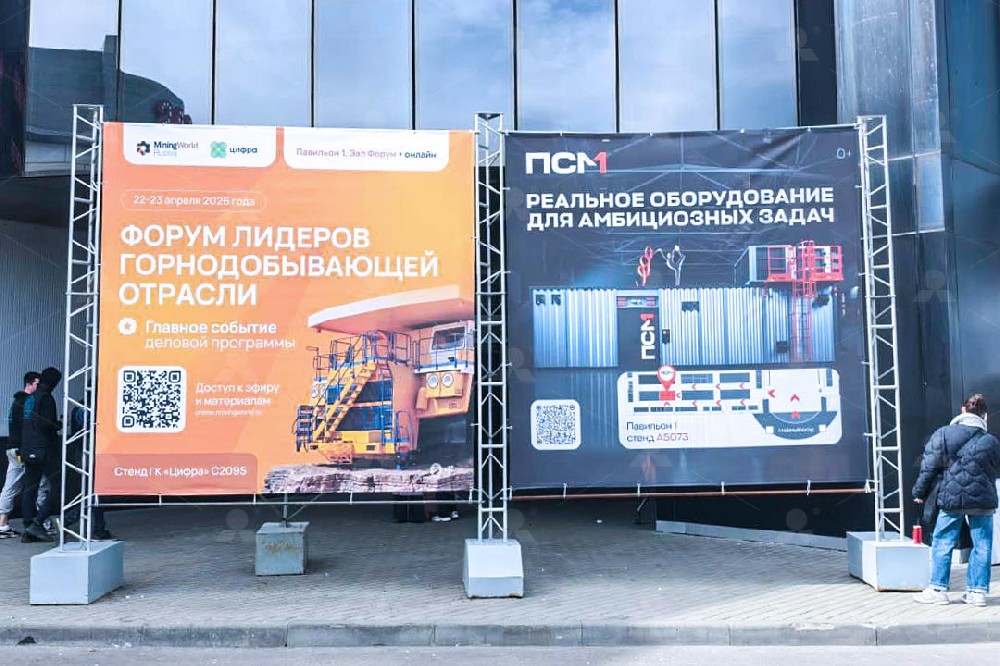
Highlights from MiningWorld Russia 2026: A Successful Showcase in Moscow

We are pleased to announce the successful conclusion of our participation in MiningWorld Russia 2026, the largest international exhibition for mining equipment, technologies, and services in Russia.

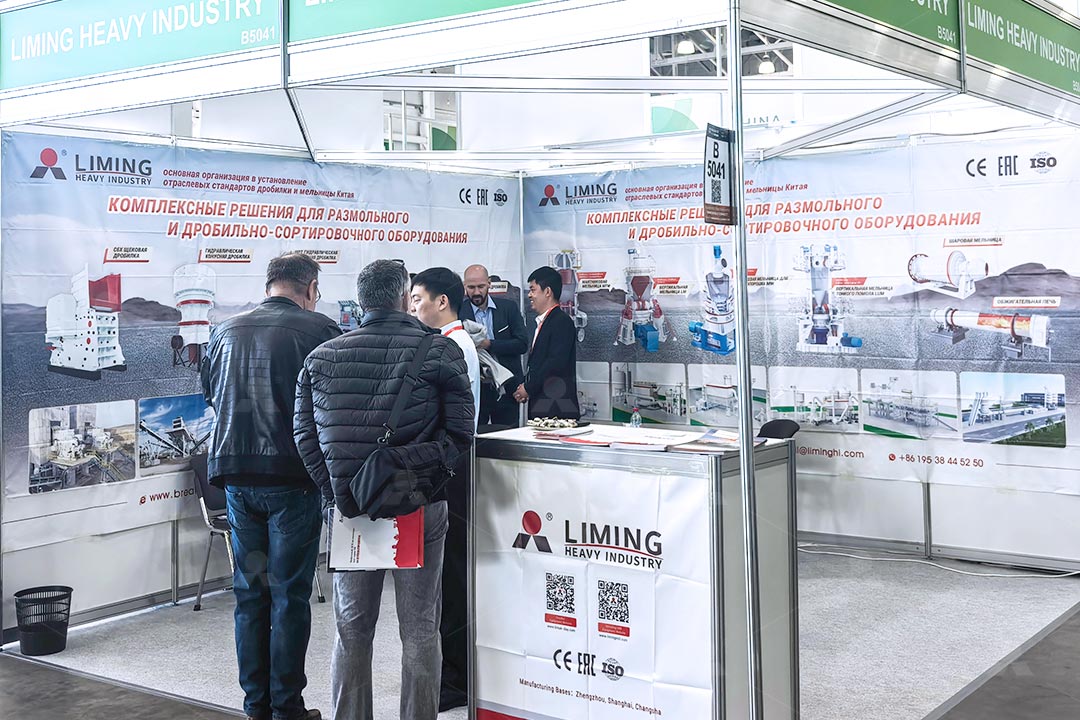
Held from April 22–24 at the Crocus Expo IEC, Pavilion 1, our team had the honor of welcoming hundreds of visitors to our booth B5041. The event provided an excellent platform to demonstrate our commitment to the mining sector and engage with key stakeholders in the industry.

Event Highlights:

  • Strong Engagement: Our technical experts held in-depth discussions with potential clients and partners regarding mining solutions.


  • Product Showcase: We displayed our core products, attracting significant interest from local mining enterprises.


  • Networking: We established valuable connections that will help us better serve the Russian market.


We are excited to share that high-resolution photos from the exhibition have just arrived! You can view the gallery [here/attached] to see the energy and excitement from our booth.

03.jpg06.jpg


Looking to Connect?

If you missed us at the show or would like to discuss business opportunities, please feel free to contact our representatives directly via WhatsApp or phone:

  • Konstantin Guo

    📱 +86 186 2558 8441


  • Sasha Du

    📱 +86 135 9883 0486


Thank you to everyone who made this event a success. We look forward to seeing you again next year!


17/4/2026

17/4/2026

Practical Ways to Reduce Operating Costs in Aggregate Crushing Plants

In today’s competitive aggregate and construction markets, profit margins are under constant pressure. While increasing production is one approach, experienced operators know that controlling operating costs is often more effective and sustainable.

Here are five proven strategies widely used in modern crushing plants.

1. Optimize the Feed Size and Gradation

Feeding oversized or uneven material into a crusher leads to:

  • Reduced efficiency

  • Increased wear

  • Higher energy consumption

Installing a proper pre-screening system can remove fine materials before crushing, allowing the crusher to focus only on what actually needs processing. This simple adjustment can improve overall efficiency by 10–15%.

2. Choose the Right Crushing Stage Configuration

A well-balanced crushing circuit reduces unnecessary load on each machine.

Typical optimized setups include:

  • Jaw + cone (for hard rock)

  • Jaw + impact (for softer materials)

  • Multi-stage crushing with screening loops

Improper configuration often results in one machine becoming a bottleneck, forcing others to operate below capacity.

3. Control Wear Parts Consumption

Wear parts are one of the largest ongoing costs in crushing operations.

To reduce replacement frequency:

  • Use the correct material grade (Mn steel, alloy, etc.)

  • Maintain consistent feed conditions

  • Avoid overloading or uneven feeding

  • Rotate liners regularly

Tracking wear life data helps predict replacement cycles and avoid emergency shutdowns.

4. Improve Automation and Monitoring

Manual operation increases the risk of human error and inconsistent performance.

Modern crushing plants increasingly use:

  • PLC control systems

  • Real-time production monitoring

  • Automatic load adjustment

These systems help maintain optimal operating conditions and reduce unnecessary energy consumption.

5. Minimize Downtime Through Preventive Maintenance

Unexpected shutdowns are often the most expensive problem.

A structured maintenance plan should include:

  • Daily inspections

  • Scheduled lubrication

  • Vibration and temperature monitoring

  • Early fault detection

Many operators underestimate how much downtime impacts profitability. In reality, even a few hours of stoppage can outweigh savings from cheaper equipment.

Conclusion

Reducing operating costs is not about cutting corners—it’s about improving efficiency at every stage of the process.

From feed control to maintenance planning, small adjustments can lead to significant savings over time. The most successful operations are those that treat cost control as a continuous process, not a one-time effort.


16/4/2026

16/4/2026

How to Choose the Right Crushing Equipment for Your Mining Project

Selecting the right crushing equipment is one of the most critical decisions in a mining project. It directly impacts production efficiency, operating costs, and long-term profitability. Yet many projects still face issues like over-investment, under-capacity, or frequent downtime—often due to poor equipment selection at the early stage.

This guide outlines the key factors that experienced operators consider before finalizing a crushing solution.

1. Understand Your Material Characteristics

Not all rocks behave the same under compression. Before choosing a crusher, you need a clear understanding of:

  • Hardness (e.g., granite vs. limestone)

  • Abrasiveness (affects wear parts consumption)

  • Moisture content (risk of clogging)

  • Feed size distribution

For example, highly abrasive materials like basalt will significantly increase liner wear in impact crushers, making jaw + cone combinations a more cost-effective choice over time.

2. Define Your Production Targets Clearly

Capacity is not just about tons per hour—it must match your actual operational conditions.

Ask yourself:

  • What is the required hourly and daily output?

  • Is production continuous or intermittent?

  • Are there peak demand periods?

A common mistake is selecting equipment based on theoretical capacity rather than real working capacity. A safety margin of 10–20% is usually recommended to handle fluctuations.

3. Determine the Final Product Requirements

End-product size and shape play a decisive role in equipment selection.

  • Coarse aggregates → Jaw crusher is sufficient

  • Medium aggregates → Cone crusher preferred

  • High-quality cubic shape (for concrete/asphalt) → Impact crusher or VSI

If your project supplies high-grade concrete, investing in shaping equipment is not optional—it directly affects your product competitiveness.

4. Consider Mobility vs. Stationary Setup

The choice between stationary and mobile crushing plants depends on project duration and site conditions.

  • Stationary plants: Suitable for long-term, high-capacity operations

  • Mobile crushers: Ideal for short-term projects, scattered sites, or urban construction

In recent years, more contractors are shifting toward mobile solutions to reduce transportation costs and improve flexibility, especially in infrastructure and demolition projects.

5. Evaluate Total Cost of Ownership (TCO)

Focusing only on initial purchase cost often leads to higher expenses later.

A proper evaluation should include:

  • Wear parts consumption

  • Energy consumption

  • Maintenance frequency

  • Downtime risk

  • Labor requirements

In many cases, a slightly higher upfront investment can reduce operating costs by 20–30% over the equipment lifecycle.

6. After-Sales Support Matters More Than You Think

Even the best equipment will require maintenance. What separates reliable suppliers from the rest is:

  • Spare parts availability

  • Technical support response time

  • Remote diagnostics capability

  • On-site service options

Delayed support can stop an entire production line—something no operator can afford.

Conclusion

Choosing the right crushing equipment is not about buying the most advanced machine—it’s about selecting a system that fits your material, production goals, and operating conditions.

A well-designed crushing solution will not only improve efficiency but also stabilize your long-term operating costs and reduce unexpected risks.


10/4/2026

10/4/2026

How to Lower Wear Parts Cost in Aggregate Plants

In aggregate production, wear parts are one of the most significant ongoing operating costs. Components such as jaw plates, cone liners, mantles, blow bars, and screen media are constantly exposed to impact, abrasion, and high-pressure loads. If not properly managed, frequent replacements can increase downtime, raise cost per ton, and reduce overall plant profitability.

The good news is that wear parts cost can be significantly reduced through proper equipment selection, optimized process design, and disciplined maintenance practices.

This article outlines practical strategies to lower wear parts costs in aggregate plants while maintaining stable output and high product quality.


1. Match the Right Equipment to the Material

One of the most common reasons for excessive wear is using equipment that is not suitable for the material.

Material-based recommendations:

  • Granite / Basalt / Hard rock
    → Jaw crusher + cone crusher
    → Avoid excessive impact crushing

  • Limestone / Soft to medium-hard rock
    → Jaw crusher + impact crusher or cone crusher

  • River stone / Abrasive aggregate
    → Compression crushing + VSI shaping (if needed)

Using the correct crusher type reduces unnecessary impact stress and extends wear part life.


2. Control Feed Size and Gradation

Improper feed conditions accelerate wear and reduce crushing efficiency.

Common problems:

  • Oversized rocks entering the crusher

  • Excessive fines causing packing

  • Uneven feed distribution

Solutions:

  • Install vibrating feeders with grizzly bars

  • Pre-screen fines before crushing

  • Maintain consistent feed size

Stable feed conditions ensure smoother crushing and more uniform liner wear.


3. Optimize Crusher Settings

Incorrect crusher settings can dramatically increase wear.

Key settings to monitor:

  • Closed Side Setting (CSS)
    Overly tight CSS increases pressure and liner wear

  • Chamber profile
    Wrong chamber design causes uneven wear

  • Crusher speed
    Excessive speed may increase abrasion

Best practice:

Adjust crusher settings based on:

  • Material hardness

  • Feed size

  • Target output

Optimized settings improve both wear life and production efficiency.


4. Improve Material Flow and Plant Layout

Poor plant layout can create bottlenecks and recirculation overload, which increase wear.

Common issues:

  • Frequent crusher overload

  • Excessive recirculating load

  • Material buildup at transfer points

Solutions:

  • Balance crusher and screen capacities

  • Improve transfer chute design

  • Use closed-circuit systems

A smooth material flow reduces unnecessary crushing cycles and wear.


5. Select High-Quality Wear Materials

Wear parts material selection has a major impact on service life.

Common wear materials:

  • High manganese steel

  • Alloy steel

  • Chrome alloys

  • Composite wear materials

Selection depends on:

  • Material hardness

  • Abrasiveness

  • Impact load

High-quality wear parts may cost more initially but often reduce total replacement frequency and downtime.


6. Implement Preventive Maintenance

Wear part management should be proactive, not reactive.

Key maintenance actions:

  • Inspect wear thickness regularly

  • Rotate liners if applicable

  • Check bolt tightness

  • Monitor vibration and noise

  • Maintain lubrication systems

A preventive maintenance plan helps detect wear issues early and avoid major failures.


7. Train Operators for Correct Crusher Operation

Operator practices directly affect wear part consumption.

Common mistakes:

  • Overfeeding

  • Uneven loading

  • Ignoring warning signs

Benefits of training:

  • Better feed control

  • Timely adjustments

  • Safer operation

Well-trained operators can significantly reduce wear-related costs.


8. Use Automation and Monitoring Systems

Modern aggregate plants increasingly use automation to optimize performance.

Useful technologies:

  • Load monitoring

  • CSS automatic adjustment

  • Wear tracking sensors

  • Predictive maintenance alerts

Automation improves consistency and helps avoid conditions that accelerate wear.


Conclusion

Lowering wear parts cost in aggregate plants requires a combination of the right equipment, optimized crushing conditions, quality wear materials, and disciplined maintenance. By improving material flow, feed control, and operator practices, aggregate producers can significantly reduce cost per ton and improve plant profitability.

A strategic approach to wear management not only saves money but also ensures more stable, efficient, and sustainable production.


  • Home
  • Prev
  • ···23456···
  • Last
Clicky